Electric Vehicles. Can anyone make this make sense?

WI_Hedgehog

Well-known member

Equipment
BX2370 (impliment details in my Profile->About)
Apr 24, 2024
1,130
1,647
113
Milwaukee, Wisconsin, U.S.A.
A36 is a hot rolled structural steel and totally fine in that application. 1020, 1018. 1045, and a host of other "mild steels" are readily available with or without CERTS.

A36 machines like crap and any shop that loads it in a machining center has only themselves to blame for the results..

Dan
Post-2020, in the Milwaukee area, in my line of work:

1020 Hot Roll is much harder to find than A36 and if found significantly more expensive. It's also not great to machine since the Frank Dodd Conflict Minerals Act was used by the EPA to remove much of the lead content (that's just my opinion, but it certainly appears to be the case). FM-15, FM-20, and Freemax (all free-machining materials) were also heavily affected (not just my opinion).


1018 is usually relegated to Cold Roll bars, and is much harder to find than A36 and if found significantly more expensive. In fact A36 Hot Roll bars are getting to come by depending on the size. Cold Roll isn't stable from my experience.

1045 is around 20% more expensive than A36 and not that readily available over 1.5", in either plate or bar.

If steel doesn't have mill certs I won't buy it, except for use in industrial large-size washing machine end plates where tight tolerances aren't required.
 

TheOldHokie

Well-known member
Lifetime Member

Equipment
L3901/LA525, G2160/RCK60, G2460/RCK60
Apr 6, 2021
13,118
7,399
113
Myersville, MD
windyridgefarm.us
Post-2020, in the Milwaukee area, in my line of work:

1020 Hot Roll is much harder to find than A36 and if found significantly more expensive. It's also not great to machine since the Frank Dodd Conflict Minerals Act was used by the EPA to remove much of the lead content (that's just my opinion, but it certainly appears to be the case). FM-15, FM-20, and Freemax (all free-machining materials) were also heavily affected (not just my opinion).


1018 is usually relegated to Cold Roll bars, and is much harder to find than A36 and if found significantly more expensive. In fact A36 Hot Roll bars are getting to come by depending on the size. Cold Roll isn't stable from my experience.

1045 is around 20% more expensive than A36 and not that readily available over 1.5", in either plate or bar.

If steel doesn't have mill certs I won't buy it, except for use in industrial large-size washing machine end plates where tight tolerances aren't required.
It sounds like your real complaint is cost and want to pinch pennies by using A36.

I am a hobbyist just outside Baltimore and can and do buy all of those steels except 1020 in rounds from my local retail service center. I buy mill lengths in hot and cold rolled 1018 rounds up to 4.5". Over that its sawed/slabbed to length. They could obviously supply mill lengths if I needed it. I also buy mill lengths of 1" 1045 TGP for shafting and its stocked in both smaller and larger sizes.

For free machining steel I buy leaded 12L14 rounds and hex bars. Its not expensive but rusts in the blink of an eye so it sees limited use. Stressproof (1144) bars are also readily available but at a very significant premium.

I dont use a lot of flats but hot and cold rolled 1018 is readily available in small to sizes way to big for my needs. I mostly use 1" and under cold rolled flats for things that require very little machining. I am looking for precision and surface finish not dimensional stability under hogging cuts.

If I were a commercial enterprise I would be buying from the main steel distributor in Baltimore. They have far more inventory but are strictly wholesale and only deal in mill lengths.

Dan
 
  • Like
Reactions: 1 user

Daferris

Well-known member

Equipment
LX2610
Nov 23, 2021
496
423
63
Mid-Michigan
Just my $0.02 on EV's. Correct they are not for everyone. But I bought a new '17 Chevy Volt ( gas/electric extended range EV). In Feb 2018. It's now 8 years old the battery in the 8 years still has 95% of it's usable capacity but I still get more than the 53 miles on a warm day out of it. New I could get it I took back roads instead of the highway 62 miles now it's 56 miles. On long trips I don't bother to charge it. It gets 45+ mpg on gas. Back when I was working I had a 36 mile round trip commute it cost me an extra $25 in my electric bill per month. The car is super cheap to drive. Yes I have other autos but only use them occasionally the Volt is the go to unless I need to haul or tow something. Also put in a solar array after I retired last spring. 16kw of bifacial panels on a seasonal adjustable ground mount and 64kWh of batteries. Started producing power in July. So far December's bill I used 82kWh from the grid and January 157kWh as I ran the batteries down to 25% and it switched to using the grid to make up power when not enough PV coming in due to clouds. I did the solar install myself and the system should be cash flow positive around August '29. Again it's not for everyone but for me it works. And now with the dual fuel heat pump that I put in in '24 I'm using less than 500 gallons of propane for heat ( under 35f) hot water and the dryer. I have a 5kw space heater that runs off solar in the winter when the batteries are above 90% SOC and I need to " burn up excess" solar does not happen as much as I would like but any either day that you can see the sun for more than 3-4 hours I have enough extra PV to run it and save some propane.
 
  • Like
Reactions: 2 users

TheOldHokie

Well-known member
Lifetime Member

Equipment
L3901/LA525, G2160/RCK60, G2460/RCK60
Apr 6, 2021
13,118
7,399
113
Myersville, MD
windyridgefarm.us
Just my $0.02 on EV's. Correct they are not for everyone. But I bought a new '17 Chevy Volt ( gas/electric extended range EV). In Feb 2018. It's now 8 years old the battery in the 8 years still has 95% of it's usable capacity but I still get more than the 53 miles on a warm day out of it. New I could get it I took back roads instead of the highway 62 miles now it's 56 miles. On long trips I don't bother to charge it. It gets 45+ mpg on gas. Back when I was working I had a 36 mile round trip commute it cost me an extra $25 in my electric bill per month. The car is super cheap to drive. Yes I have other autos but only use them occasionally the Volt is the go to unless I need to haul or tow something. Also put in a solar array after I retired last spring. 16kw of bifacial panels on a seasonal adjustable ground mount and 64kWh of batteries. Started producing power in July. So far December's bill I used 82kWh from the grid and January 157kWh as I ran the batteries down to 25% and it switched to using the grid to make up power when not enough PV coming in due to clouds. I did the solar install myself and the system should be cash flow positive around August '29. Again it's not for everyone but for me it works. And now with the dual fuel heat pump that I put in in '24 I'm using less than 500 gallons of propane for heat ( under 35f) hot water and the dryer. I have a 5kw space heater that runs off solar in the winter when the batteries are above 90% SOC and I need to " burn up excess" solar does not happen as much as I would like but any either day that you can see the sun for more than 3-4 hours I have enough extra PV to run it and save some propane.
One might be tempted to think widespread deployment of rooftop/ground array PV solar could power structures and supply a significant decentralized backfeed into the grid for redistribution.

NAH - thats got to be fantasy.

Dan
 
Last edited:
  • Like
Reactions: 1 user

WI_Hedgehog

Well-known member

Equipment
BX2370 (impliment details in my Profile->About)
Apr 24, 2024
1,130
1,647
113
Milwaukee, Wisconsin, U.S.A.
It sounds like your real complaint is cost and want to pinch pennies by using A36.

I am a hobbyist just outside Baltimore and can and do buy all of those steels except 1020 in rounds from my local retail service center. I buy mill lengths in hot and cold rolled 1018 rounds up to 4.5". Over that its sawed/slabbed to length. They could obviously supply mill lengths if I needed it. I also buy mill lengths of 1" 1045 TGP for shafting and its stocked in both smaller and larger sizes.

For free machining steel I buy leaded 12L14 rounds and hex bars. Its not expensive but rusts in the blink of an eye so it sees limited use. Stressproof (1144) bars are also readily available but at a very significant premium.

I dont use a lot of flats but hot and cold rolled 1018 is readily available in small to sizes way to big for my needs. I mostly use 1" and under cold rolled flats for things that require very little machining. I am looking for precision and surface finish not dimensional stability under hogging cuts.

If I were a commercial enterprise I would be buying from the main steel distributor in Baltimore. They have far more inventory but are strictly wholesale and only deal in mill lengths.

Dan
It sounds like you go through an impressive amount of steel for a hobbyist! That's awesome, as is the availability of materials.

I'll give you this as background, not being competitive at all--you'd win that in my book because building your own stuff is way more fun than building someone else's stuff.

It's a little long but sheds a lot of light on why that one OTT member-and maybe others-think Engineers are morons.

AND I think most people can appreciate this having experienced something similar themselves.

I'm also going to use a bunch of stereotypes and generalizations because who doesn't find social conflict entertaining?
---

Fabrication in Milwaukee is highly competitive, so "shopping a job" is a given, especially nowadays; years ago companies used to form relationships and as a fabricator I knew what a customers needs were and would catch mistakes and find affordable ways to give them what they wanted.

To "save money" companies "let go" the older, "expensive" engineers (the people who knew what they were doing), replacing them with middle-managers ("the boss" who thinks he knows what he's doing) and eventually replacing them with "purchasing agents" who in reality are mainly office girls who want to do nothing more than move a stack of papers from one side of their desk (to-do) to the other (done)--they have no idea what they need or what a job is used for, which is an issue, and you're about to see why.

Instead of a customer supplying Fabrication and Machining prints I get machining prints with everything dimensioned to three places so I don't know if they really need +/-0.001", Flat/Parallel within 0.002" over 8 feet or not (those tolerances over 6" would be fine, but much of this stuff is much, much bigger), and the office girl doesn't know either but she can ask the fresh out of college kid who drew it (they won't let you talk to "designers" directly because they're saving costs by having the blonde manage the phone), though he has no idea what +/-.001 costs compared to +/-.025 or what tolerances are needed because the company "let go" everyone with that experience long before the kid was hired.

Since nobody really knows what the thing does or how it should do it, it's all about cost.

If Fabricator #2 can save the customer $1,000 with +/-.030" vs. me at +/-.010" they'll go with #2, because the office girl only knows #2 costs $1,000 less. In her eyes someone above her should have caught the "whatever thing" wouldn't work, or someone after her has to find a way to make it work, she did the paperwork fast and "saved the company money." The end result is fabricators quote as loose as they think they can without looking stupid.

You mention pinching pennies. Much of what we build is around 1,000-5,000#, each, so steel is bought by the semi-load. A sheet of steel is 8' x 20', so 1" thick plate (the thin stuff) is about 6,500#, and steel is priced by cost-per-100-pounds (CWT, cost per hundred weight). With that in mind, 1020 & 1018 HR steel isn't usually stocked at the local service centers, it's A36, and for good reason.

1020/1018 is a virgin steel product (unlike your first girlfriend, at least by the time you got done with her), and mining in the U.S. is "pretty much banned" because of environmental regulations. Without raw materials we need to recycle existing material, which is what A36 is, recycled "stuff." Push the car, toaster, stapler, pitchfork into the vat, get steel out, that's the concept. It's not stable like virgin steel (think of that redhead you dated--fun but not exactly "stable" and definitely not "virgin") which is iron ore and a few additives, but it does look about the same from six feet away....

1045 plate is usually stocked up to 1-1/2", sometimes I can get up to 3-3/4", sometimes. The price is about 80% more than A36 (300% more for the thick stuff), so when Customer #1 is shopping Fabricator #1 against Fabricator #2 do you think she's going to choose the fabricator who will do the job for $35,000 or the fabricator who will do it for $20,000? I'm going to tell you, every single time it's the guy using A36, which is why 1020/1018 is hardly stocked here and 1045 hit-and-miss.

4140 is stocked in major increments, not 1/8" increments, and heavier stuff is regularly on backorder, it's about 5x the price of A36. Free-machining material is about 4x and in 1/8" increments up to 1-1/2", though without the lead content it's not worth it. 12L14 is available in very limited sizes and is spendy, so I can't really use it for building anything sizeable.

---

Plastic quality is "somewhat similar," good plastic is expensive, cutting corners saves money and is easy to make in volume for Walmart shoppers. (And you know it's true because that's why people shop Temu.) And that's why your toaster, car, kitchen utensils, and girlfriend have cheap plastic and don't last long.

Metal lasts longer and is stronger (like your wife, works hard and not too emotional). BUT, quality costs more, and there's only so much money to go around, which is why we're not all married to supermodels.

1770736227925.png
 

TheOldHokie

Well-known member
Lifetime Member

Equipment
L3901/LA525, G2160/RCK60, G2460/RCK60
Apr 6, 2021
13,118
7,399
113
Myersville, MD
windyridgefarm.us
It sounds like you go through an impressive amount of steel for a hobbyist! That's awesome, as is the availability of materials.

I'll give you this as background, not being competitive at all--you'd win that in my book because building your own stuff is way more fun than building someone else's stuff.

It's a little long but sheds a lot of light on why that one OTT member-and maybe others-think Engineers are morons.

AND I think most people can appreciate this having experienced something similar themselves.

I'm also going to use a bunch of stereotypes and generalizations because who doesn't find social conflict entertaining?
---

Fabrication in Milwaukee is highly competitive, so "shopping a job" is a given, especially nowadays; years ago companies used to form relationships and as a fabricator I knew what a customers needs were and would catch mistakes and find affordable ways to give them what they wanted.

To "save money" companies "let go" the older, "expensive" engineers (the people who knew what they were doing), replacing them with middle-managers ("the boss" who thinks he knows what he's doing) and eventually replacing them with "purchasing agents" who in reality are mainly office girls who want to do nothing more than move a stack of papers from one side of their desk (to-do) to the other (done)--they have no idea what they need or what a job is used for, which is an issue, and you're about to see why.

Instead of a customer supplying Fabrication and Machining prints I get machining prints with everything dimensioned to three places so I don't know if they really need +/-0.001", Flat/Parallel within 0.002" over 8 feet or not (those tolerances over 6" would be fine, but much of this stuff is much, much bigger), and the office girl doesn't know either but she can ask the fresh out of college kid who drew it (they won't let you talk to "designers" directly because they're saving costs by having the blonde manage the phone), though he has no idea what +/-.001 costs compared to +/-.025 or what tolerances are needed because the company "let go" everyone with that experience long before the kid was hired.

Since nobody really knows what the thing does or how it should do it, it's all about cost.

If Fabricator #2 can save the customer $1,000 with +/-.030" vs. me at +/-.010" they'll go with #2, because the office girl only knows #2 costs $1,000 less. In her eyes someone above her should have caught the "whatever thing" wouldn't work, or someone after her has to find a way to make it work, she did the paperwork fast and "saved the company money." The end result is fabricators quote as loose as they think they can without looking stupid.

You mention pinching pennies. Much of what we build is around 1,000-5,000#, each, so steel is bought by the semi-load. A sheet of steel is 8' x 20', so 1" thick plate (the thin stuff) is about 6,500#, and steel is priced by cost-per-100-pounds (CWT, cost per hundred weight). With that in mind, 1020 & 1018 HR steel isn't usually stocked at the local service centers, it's A36, and for good reason.

1020/1018 is a virgin steel product (unlike your first girlfriend, at least by the time you got done with her), and mining in the U.S. is "pretty much banned" because of environmental regulations. Without raw materials we need to recycle existing material, which is what A36 is, recycled "stuff." Push the car, toaster, stapler, pitchfork into the vat, get steel out, that's the concept. It's not stable like virgin steel (think of that redhead you dated--fun but not exactly "stable" and definitely not "virgin") which is iron ore and a few additives, but it does look about the same from six feet away....

1045 plate is usually stocked up to 1-1/2", sometimes I can get up to 3-3/4", sometimes. The price is about 80% more than A36 (300% more for the thick stuff), so when Customer #1 is shopping Fabricator #1 against Fabricator #2 do you think she's going to choose the fabricator who will do the job for $35,000 or the fabricator who will do it for $20,000? I'm going to tell you, every single time it's the guy using A36, which is why 1020/1018 is hardly stocked here and 1045 hit-and-miss.

4140 is stocked in major increments, not 1/8" increments, and heavier stuff is regularly on backorder, it's about 5x the price of A36. Free-machining material is about 4x and in 1/8" increments up to 1-1/2", though without the lead content it's not worth it. 12L14 is available in very limited sizes and is spendy, so I can't really use it for building anything sizeable.

---

Plastic quality is "somewhat similar," good plastic is expensive, cutting corners saves money and is easy to make in volume for Walmart shoppers. (And you know it's true because that's why people shop Temu.) And that's why your toaster, car, kitchen utensils, and girlfriend have cheap plastic and don't last long.

Metal lasts longer and is stronger (like your wife, works hard and not too emotional). BUT, quality costs more, and there's only so much money to go around, which is why we're not all married to supermodels.

View attachment 169632
So in summary you are loosening tolerances and using A36 over more desirable but expensive grades to shave costs and win bids. If that passes muster with the customer's decision maker in chief I guess thats fine. I have helped write and evaluate bids on more than one multi-million dollar RFP and playing fast and loose with specifications would never have survived our review process.

Over specification is always a concern which is why major RFPs were typically preceded by one or more RFC's and vendor feedback was incorporated into the RFP so ALL bidders were competing on even terms.

In any event bitching about the machining quality of your material of choice which is fundamentally produced as a structural steel seems upside down.

And how any of this relates to EVs is a total mystery to me.
 
Last edited:
  • Haha
  • Like
Reactions: 1 users

WI_Hedgehog

Well-known member

Equipment
BX2370 (impliment details in my Profile->About)
Apr 24, 2024
1,130
1,647
113
Milwaukee, Wisconsin, U.S.A.
So in summary you are loosening tolerances and using A36 over more desirable but expensive grades to shave costs and win bids. If that passes muster with the customer's decision maker in chief I guess thats fine. I have helped write and evaluate bids on more than one multi-million dollar RFP and playing fast and loose with specifications would never have survived our review process.

Over specification is always a concern which is why major RFPs were typically preceded by one or more RFC's and vendor feedback was incorporated into the RFP so ALL bidders were competing on even terms.

In any event bitching about the machining quality of your material of choice which is fundamentally produced as a structural steel seems upside down.

And how any of this relates to EVs is a total mystery to me.
Yup. Let's say they want a robot pedestal to 36" high x 24" square +/-.001" F/P .001 [16 microFinish]. I asked them, "How are you mounting it to the concrete floor?" They don't know. I asked, "How is it you need it 36" high, +/-.001? Are you using precision adjusters and calibrated laser levels?"

Customer: "We're just bolting it to the floor."

Me: "Straight to the floor?"

Them: "Yeah, why?"

Me: "Wellll....you toleranced the bolt holes as reamed +/-2 tenths, aligned with the top holes within 2 tenths, and I'm thinking that might be a bit unnecessary if you're drilling holes in concrete and using lags to bolt it down." (note for those who don't know, that's a hole diameter within 2 tenths of 1 thousandth of an inch, not 0.2 inches, so the hole diameter is about 25 times more accurate than "within the thickness of a human hair")

Them: "Oh, what do you think it should be?"

Me: "What are you laying out the holes with?"

Them: "What do you mean?"

Me: Are you using a tape measure and felt-tip marker to mark the holes on the concrete?

Them: No, we thought we'd drill through the holes you put in so we put the holes in the right spot.

Me: How do you know the location of the robot compared to the existing equipment?

Them: Well, we have an open space next to the, the, um, I'll text you a picture...

---
So yeah, building it to print is $175 per hole that they're going to use as a drill guide, then put a concrete lag through, ...or I could just drill it. They should use levelers anyway, but "not my problem."
---

Back on topic, remember when Elon set up a sleeping cot at the end of the automated production line that couldn't get the car doors on straight when they turned the line up to full speed? (And there were other issues, but that's the one car guys took notice of because some car doors wouldn't close.) We built part of the solution, and he could go back to sleeping on a random friend's couch. So what we do isn't actually "slop," we know how to make things work "affordably," and some of it has to do with EVs.

And some of it has to do with sales calls to those blonde buyers and making them look good--it's a tough job, but somebody has to do it.

1770745895769.png
 

TheOldHokie

Well-known member
Lifetime Member

Equipment
L3901/LA525, G2160/RCK60, G2460/RCK60
Apr 6, 2021
13,118
7,399
113
Myersville, MD
windyridgefarm.us
Yup. Let's say they want a robot pedestal to 36" high x 24" square +/-.001" F/P .001 [16 microFinish]. I asked them, "How are you mounting it to the concrete floor?" They don't know. I asked, "How is it you need it 36" high, +/-.001? Are you using precision adjusters and calibrated laser levels?"

Customer: "We're just bolting it to the floor."

Me: "Straight to the floor?"

Them: "Yeah, why?"

Me: "Wellll....you toleranced the bolt holes as reamed +/-2 tenths, aligned with the top holes within 2 tenths, and I'm thinking that might be a bit unnecessary if you're drilling holes in concrete and using lags to bolt it down." (note for those who don't know, that's a hole diameter within 2 tenths of 1 thousandth of an inch, not 0.2 inches, so the hole diameter is about 25 times more accurate than "within the thickness of a human hair")

Them: "Oh, what do you think it should be?"

Me: "What are you laying out the holes with?"

Them: "What do you mean?"

Me: Are you using a tape measure and felt-tip marker to mark the holes on the concrete?

Them: No, we thought we'd drill through the holes you put in so we put the holes in the right spot.

Me: How do you know the location of the robot compared to the existing equipment?

Them: Well, we have an open space next to the, the, um, I'll text you a picture...

---
So yeah, building it to print is $175 per hole that they're going to use as a drill guide, then put a concrete lag through, ...or I could just drill it. They should use levelers anyway, but "not my problem."
---

Back on topic, remember when Elon set up a sleeping cot at the end of the automated production line that couldn't get the car doors on straight when they turned the line up to full speed? (And there were other issues, but that's the one car guys took notice of because some car doors wouldn't close.) We built part of the solution, and he could go back to sleeping on a random friend's couch. So what we do isn't actually "slop," we know how to make things work "affordably," and some of it has to do with EVs.

And some of it has to do with sales calls to those blonde buyers and making them look good--it's a tough job, but somebody has to do it.

View attachment 169643
So that (hypothetical ??) customer is staffed with engineerimg morons and you are supplying a consulting service.. Not unusual but one has to question the quality of the products they control and make with those robots.

If that is representative of your customers it speaks very poorly of manufacturing in WI.

But we continue to digress....
 

WI_Hedgehog

Well-known member

Equipment
BX2370 (impliment details in my Profile->About)
Apr 24, 2024
1,130
1,647
113
Milwaukee, Wisconsin, U.S.A.
So that (hypothetical ??) customer is staffed with engineerimg morons and you are supplying a consulting service.. Not unusual but one has to question the quality of the products they control and make with those robots.

If that is representative of your customers it speaks very poorly of manufacturing in WI.

But we continue to digress....
That actually happened, and eventually the robot installer called because the table was outside the robot's ability to self-level, and the company bowed the baseplate when they wrenched it down. We built them another one rush and provided many more robot stands to that company; through word-of-mouth we gained several new customers as the company that builds robot stands "that work." Win-win.

We build parts of machines that ship around the world, and you'd maybe be surprised which giant companies employ green college kids straight off the turnip truck as their primary workforce. Trial by Fire! šŸ˜„ It's brutal.

---
We still have:
  • Komatsu (giant excavation equipment)
  • P&H (giant excavation equipment)
  • Briggs & Stratton (engines)
  • GE Healthcare (the first MRI was built here)
  • Harley-Davidson (motorcycles)
  • Milwaukee Electric Tool
  • Snap-on Tools
  • Rockwell Automation
  • Oshkosh Truck (the military vehicle guys)
  • Generac (generators)
  • Brady Corporation (the label maker guys)
  • A.O. Smith (water heaters/treatment)
  • STRATTEC Security Corporation (automotive)
  • Manitowoc Crane
  • Mercury Marine
  • Johnson Controls
  • Regal Rexnord (electric motors)
  • Douglas Dynamics
  • John Deere (we make a bunch of their machinery here)
  • Red Star Yeast
  • Patric Cudahy (the bacon makers!)
  • Tombstone Pizza
  • Quad Graphics
and many more, so manufacturing in Wisconsin is maybe something you might have heard of. Maybe.

We also have a fair amount of railroad and automotive machinery manufacturing equipment design and construction here (still), and build things for EV manufacturers (they don't build robots in Detroit!), which you might have guessed from all the automation companies. And a bunch of hydroelectric stuff.


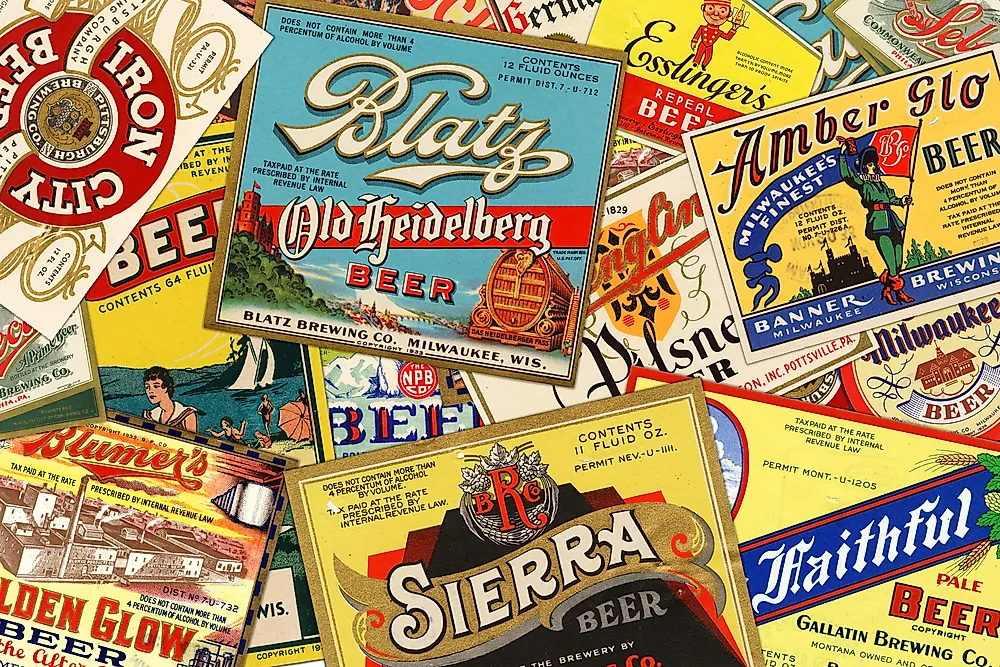
And beer. Milwaukee is known as The Beer Capitol of the World. Germanfest is held here, at which the STIHL Timbersports US Championship is held (which I regularly attend).


1770750361691.png
 
Last edited:

jimh406

Well-known member
Lifetime Member

Equipment
Kubota L2501 with R4 tires
Jan 29, 2021
3,000
2,372
113
Western MT
And beer. Milwaukee is known as The Beer Capitol of the World. Germanfest is held here, at which the STIHL Timbersports US Championship is held (which I regularly attend).
I'm not sure about Beer Capitol of the World. It is for one type of beer. ;). Fwiw, that's one of the types I don't like very much. I'm a weird one. I didn't start drinking beer very much until later in life, and my favorite now is Citra Little Thing which is about as far from Wisconsin beer as you probably can get.
 

WI_Hedgehog

Well-known member

Equipment
BX2370 (impliment details in my Profile->About)
Apr 24, 2024
1,130
1,647
113
Milwaukee, Wisconsin, U.S.A.
I'm not sure about Beer Capitol of the World. It is for one type of beer. ;). Fwiw, that's one of the types I don't like very much. I'm a weird one. I didn't start drinking beer very much until later in life, and my favorite now is Citra Little Thing which is about as far from Wisconsin beer as you probably can get.
If you didn't read the links above that's fine, but Milwaukee is also known for both making and consuming more beer in one year than the entire country of Germany.* We have micro-breweries everywhere. And when I travel and try to participate in a beer drinking contest and they find out where I'm from (the accent gives it away) they disqualify me because..."You don't drink for sport, you drink because the beer is free. When you finish one beer you ask for another."

"Milwaukee has been home to over 70 breweries and over 100 brewing companies throughout the course of its history."

Milwaukee Electric Tool Headquarters, quite the sight at night:
1770753771045.png

1770753793552.png

1770753816772.png

*I don't know that's true, but I've heard it several times throughout the years. It makes for a good story anyway.
 

TheOldHokie

Well-known member
Lifetime Member

Equipment
L3901/LA525, G2160/RCK60, G2460/RCK60
Apr 6, 2021
13,118
7,399
113
Myersville, MD
windyridgefarm.us
That actually happened, and eventually the robot installer called because the table was outside the robot's ability to self-level, and the company bowed the baseplate when they wrenched it down. We built them another one rush and provided many more robot stands to that company; through word-of-mouth we gained several new customers as the company that builds robot stands "that work." Win-win.

We build parts of machines that ship around the world, and you'd maybe be surprised which giant companies employ green college kids straight off the turnip truck as their primary workforce. Trial by Fire! šŸ˜„ It's brutal.

---
We still have Komatsu, P&H, Briggs & Stratton, GE Healthcare (the first MRI was built here), Harley-Davidson, Milwaukee Tool, Snap-on, Rockwell Automation, Oshkosh Truck (the military vehicle guys), Generac, Brady Corporation (the label maker guys), A.O. Smith (water heaters/treatment), STRATTEC Security Corporation (automotive), Manitowoc Crane, Mercury Marine, Johnson Controls, Regal Rexnord (electric motors), Douglas Dynamics, John Deere (we make a bunch of their machinery here), Red Star Yeast, Patric Cudahy (the bacon makers!), Tombstone Pizza, Quad Graphics, and many more, so manufacturing in Wisconsin is maybe something you might have heard of. Maybe.

We also have a fair amount of railroad and automotive machinery manufacturing equipment design and construction here (still), and build things for EV manufacturers (they don't build robots in Detroit!), which you might have guessed from all the automation companies. And a bunch of hydroelectric stuff.

And beer. Milwaukee is known as The Beer Capitol of the World. Germanfest is held here, where the STIHL Timbersports US Championship is held (which I regularly attend).


View attachment 169645
Do the green engineers at all of these big name companies routinely send you prints with no material specifications?

Your complaints about A36 machinability and the suggestion you could gain a competitive advantage by using a lower grade steel than your competitors is the part that started this digression. I still dont understand how that fits into the picture you are painting.

EXAMPLE

Here I am - untrained hobbiest and I need a small lot of 100 steel drive shafts made. Real simple - three diameters less than an inch over a 5" length with a .625" female hub and blind keyway on one end. One stabdard snap ring groove at the end with the hub. So I fire up Autocad and produce a print for my RFQ.

First thing in the notes block is material - 1045 steel

Next all dimensions +/- .005 unless otherwise specified.

Third a full scale dimensioned side view showing one diameter for mounting a 6063 ball bearing toleranced at +.002/-.000

Fourth a second diameter for a helical gear toleranced at +.001/-.000.

Fifth - an endview detail showing the hub and ID toleranced to +.001/-.000.

Lastly a dimensioned keyway detail toleranced at +.001/-.000 based on ANSI dimensions from my ancient copy of Machinerys Handbook and micrometer measurements of the commercially produced mating parts.

All very amateurish but nobody I send it to takes exception and thats what I expect to get

Thats a real example and the shop did a fine job with one exception. The keyway on ~20 of the pieces was undercut by a couple thousandths and the hubs would not mate to the shafts on the OTS hydraulic pumps they were meant to drive. The supplier attributed it to tool wear and I believe them. They apologised and since I did not specify any gaging requirements they gave me a small refund and I filed the keys on my pumps as needed to get them to mate.

My point is as green and lacking in formal training as I am I managed to use a little common sense and avoid basic mistakes that should be covered in Mechanical Engineering 101.

But again we digress.

Dan
 

WI_Hedgehog

Well-known member

Equipment
BX2370 (impliment details in my Profile->About)
Apr 24, 2024
1,130
1,647
113
Milwaukee, Wisconsin, U.S.A.
Do the green engineers at all of these big name companies routinely send you prints with no material specifications?

Your complaints about A36 machinability and the suggestion you could gain a competitive advantage by using a lower grade steel than your competitors is the part that started this digression. I still dont understand how that fits into the picture you are painting.

EXAMPLE

Here I am - untrained hobbiest and I need a small lot of 100 steel drive shafts made. Real simple - three diameters less than an inch over a 5" length with a .625" female hub and blind keyway on one end. One stabdard snap ring groove at the end with the hub. So I fire up Autocad and produce a print for my RFQ.

First thing in the notes block is material - 1045 steel

Next all dimensions +/- .005 unless otherwise specified.

Third a full scale dimensioned side view showing one diameter for mounting a 6063 ball bearing toleranced at +.002/-.000

Fourth a second diameter for a helical gear toleranced at +.001/-.000.

Fifth - an endview detail showing the hub and ID toleranced to +.001/-.000.

Lastly a dimensioned keyway detail toleranced at +.001/-.000 based on ANSI dimensions from my ancient copy of Machinerys Handbook and micrometer measurements of the commercially produced mating parts.

All very amateurish but nobody I send it to takes exception and thats what I expect to get

Thats a real example and the shop did a fine job with one exception. The keyway on ~20 of the pieces was undercut by a couple thousandths and the hubs would not mate to the shafts on the OTS hydraulic pumps they were meant to drive. The supplier attributed it to tool wear and I believe them. They apologised and since I did not specify any gaging requirements they gave me a small refund and I filed the keys on my pumps as needed to get them to mate.

My point is as green and lacking in formal training as I am I managed to use a little common sense and avoid basic mistakes that should be covered in Mechanical Engineering 101.

But again we digress.

Dan
I hope I didn't sound like I'm complaining, I really enjoy my job and hobbies. Things change, I adapt, it's inevitable. I try to help people and customers where possible, it's a small, small world. (Not that customers aren't people...though some days are challenging....)

---
I think the disconnect is based on scale.

For shafts, locks, keys, clamps, (sensors, actuators, indicators, panels, buttons, controllers, switches, etc.) we'd use off-the-shelf parts. If we needed custom shafts our neighbor specializes in those and OD/ID grinding.

(I think you're describing making parts.)

If you needed a machine to:
  • hammer-forge and temper tubing at high speed because you sell tubing in volume
  • manufacture clamps, sensors, actuators, etc. in high volume
  • make the paper container fries are put in (at a chain restaurant)
or you needed a work-holding fixture for turret machining center:
  • because your mining equipment manufacturing company is bolting up 3 carburetors per side, and the fixture has 3 or 4 sides, so you load 9 or 12 carburetors into a machining center at a time), and you needed 4 or 6 fixtures to run 24/7
  • because your lawn mower manufacturing company needs to machine 40 sand-castings per load
  • your tractor manufacturing company re-designed a [classified] and needs a new work-holding fixture for making a big run of the new part
or your generator company needs a press to assemble the new generator you're coming out with...

(so you're making thousands to millions of the same "thing"),

that's more along the lines of what we do. Except we're farther up the production line.
 

TheOldHokie

Well-known member
Lifetime Member

Equipment
L3901/LA525, G2160/RCK60, G2460/RCK60
Apr 6, 2021
13,118
7,399
113
Myersville, MD
windyridgefarm.us
I hope I didn't sound like I'm complaining, I really enjoy my job and hobbies. Things change, I adapt, it's inevitable. I try to help people and customers where possible, it's a small, small world. (Not that customers aren't people...though some days are challenging....)

---
I think the disconnect is based on scale.

For shafts, locks, keys, clamps, (sensors, actuators, indicators, panels, buttons, controllers, switches, etc.) we'd use off-the-shelf parts. If we needed custom shafts our neighbor specializes in those and OD/ID grinding.

(I think you're describing making parts.)

If you needed a machine to:
  • hammer-forge and temper tubing at high speed because you sell tubing in volume
  • manufacture clamps, sensors, actuators, etc. in high volume
  • make the paper container fries are put in (at a chain restaurant)
or you needed a work-holding fixture for turret machining center:
  • because your mining equipment manufacturing company is bolting up 3 carburetors per side, and the fixture has 3 or 4 sides, so you load 9 or 12 carburetors into a machining center at a time), and you needed 4 or 6 fixtures to run 24/7
  • because your lawn mower manufacturing company needs to machine 40 sand-castings per load
  • your tractor manufacturing company re-designed a [classified] and needs a new work-holding fixture for making a big run of the new part
or your generator company needs a press to assemble the new generator you're coming out with...

(so you're making thousands to millions of the same "thing"),

that's more along the lines of what we do. Except we're farther up the production line.
I think the disconnect is much more basic and has nothing to do with scale. I also think its time to put this to bed.

Dsn
 
Last edited:

GreensvilleJay

Well-known member

Equipment
BX23-S,57 A-C D-14,
Apr 2, 2019
13,904
6,331
113
Greensville,Ontario,Canada
curious about this....
Heating systems on most EV's, what you so called super efficient electric heat, well isn't very efficient!

just how do they heat your EV ? I'd assume they have a computer,sensing a SS temp chip then doing PWM to the heating element so well over 98% effiicient. it'd be nice to see the 'wiring diagram'.
 

PoTreeBoy

Well-known member
Lifetime Member

Equipment
L35 Ford 3930
Mar 24, 2020
4,077
2,514
113
WestTn/NoMs
curious about this....
Heating systems on most EV's, what you so called super efficient electric heat, well isn't very efficient!

just how do they heat your EV ? I'd assume they have a computer,sensing a SS temp chip then doing PWM to the heating element so well over 98% effiicient. it'd be nice to see the 'wiring diagram'.
Again, the heater is very efficient but the juice in the battery was produced at maybe 40% of the prime energy, assuming conventional power generation. Whereas my conventional vehicle is heated with free heat which would otherwise be wasted via the radiator.
 
  • Like
Reactions: 1 user

North Idaho Wolfman

Moderator
Staff member
Lifetime Member

Equipment
L3450DT-GST, Woods FEL, B7100 HSD, FEL, 60" SB, 743 Bobcat with V2203, and more
Jun 9, 2013
36,623
11,355
113
Sandpoint, ID
That actually happened, and eventually the robot installer called because the table was outside the robot's ability to self-level, and the company bowed the baseplate when they wrenched it down. We built them another one rush and provided many more robot stands to that company; through word-of-mouth we gained several new customers as the company that builds robot stands "that work." Win-win.

We build parts of machines that ship around the world, and you'd maybe be surprised which giant companies employ green college kids straight off the turnip truck as their primary workforce. Trial by Fire! šŸ˜„ It's brutal.

---
We still have:
  • Komatsu (giant excavation equipment)
  • P&H (giant excavation equipment)
  • Briggs & Stratton (engines)
  • GE Healthcare (the first MRI was built here)
  • Harley-Davidson (motorcycles)
  • Milwaukee Electric Tool
  • Snap-on Tools
  • Rockwell Automation
  • Oshkosh Truck (the military vehicle guys)
  • Generac (generators)
  • Brady Corporation (the label maker guys)
  • A.O. Smith (water heaters/treatment)
  • STRATTEC Security Corporation (automotive)
  • Manitowoc Crane
  • Mercury Marine
  • Johnson Controls
  • Regal Rexnord (electric motors)
  • Douglas Dynamics
  • John Deere (we make a bunch of their machinery here)
  • Red Star Yeast
  • Patric Cudahy (the bacon makers!)
  • Tombstone Pizza
  • Quad Graphics
and many more, so manufacturing in Wisconsin is maybe something you might have heard of. Maybe.

We also have a fair amount of railroad and automotive machinery manufacturing equipment design and construction here (still), and build things for EV manufacturers (they don't build robots in Detroit!), which you might have guessed from all the automation companies. And a bunch of hydroelectric stuff.


And beer. Milwaukee is known as The Beer Capitol of the World. Germanfest is held here, at which the STIHL Timbersports US Championship is held (which I regularly attend).


View attachment 169645
Your statements are full of holes!

1770778350934.png
 

Hugo Habicht

Well-known member
Lifetime Member

Equipment
G1900
Jun 24, 2024
1,542
2,238
113
Ireland
just how do they heat your EV ? I'd assume they have a computer,sensing a SS temp chip then doing PWM to the heating element so well over 98% effiicient. it'd be nice to see the 'wiring diagram'.
Burning electricity is 100% efficient, of course, but it also drains your battery dramatically. That's why manufacturers use heat pumps for the heating system.

Our postman has a battery car for a while now. Specified range is 150km. His daily round is 67km. He told me in winter he has to switch off the heating after half his round, otherwise he won't make it.
 
  • Like
Reactions: 1 user

Hugo Habicht

Well-known member
Lifetime Member

Equipment
G1900
Jun 24, 2024
1,542
2,238
113
Ireland
But I bought a new '17 Chevy Volt ( gas/electric extended range EV). In Feb 2018. It's now 8 years old the battery in the 8 years still has 95% of it's usable capacity but I still get more than the 53 miles on a warm day out of it.
Keep in mind that battery car manufacturers have extra battery capacity in the car that they do not show you. This is done to cover up the battery degradation starting with the very first charge discharge cycle. Towards the end, when this extra capacity is used up, the range drops fairly quickly.

The number of cycles at this stage exceeds typically the vehicle life expectancy but if you fast charge your battery and do deep cycles (0-100%) this changes very quickly.
 
  • Like
Reactions: 1 users